Chemical Reactor Manufacturer, Supplier & Exporter in India
What is a Chemical Reactor?
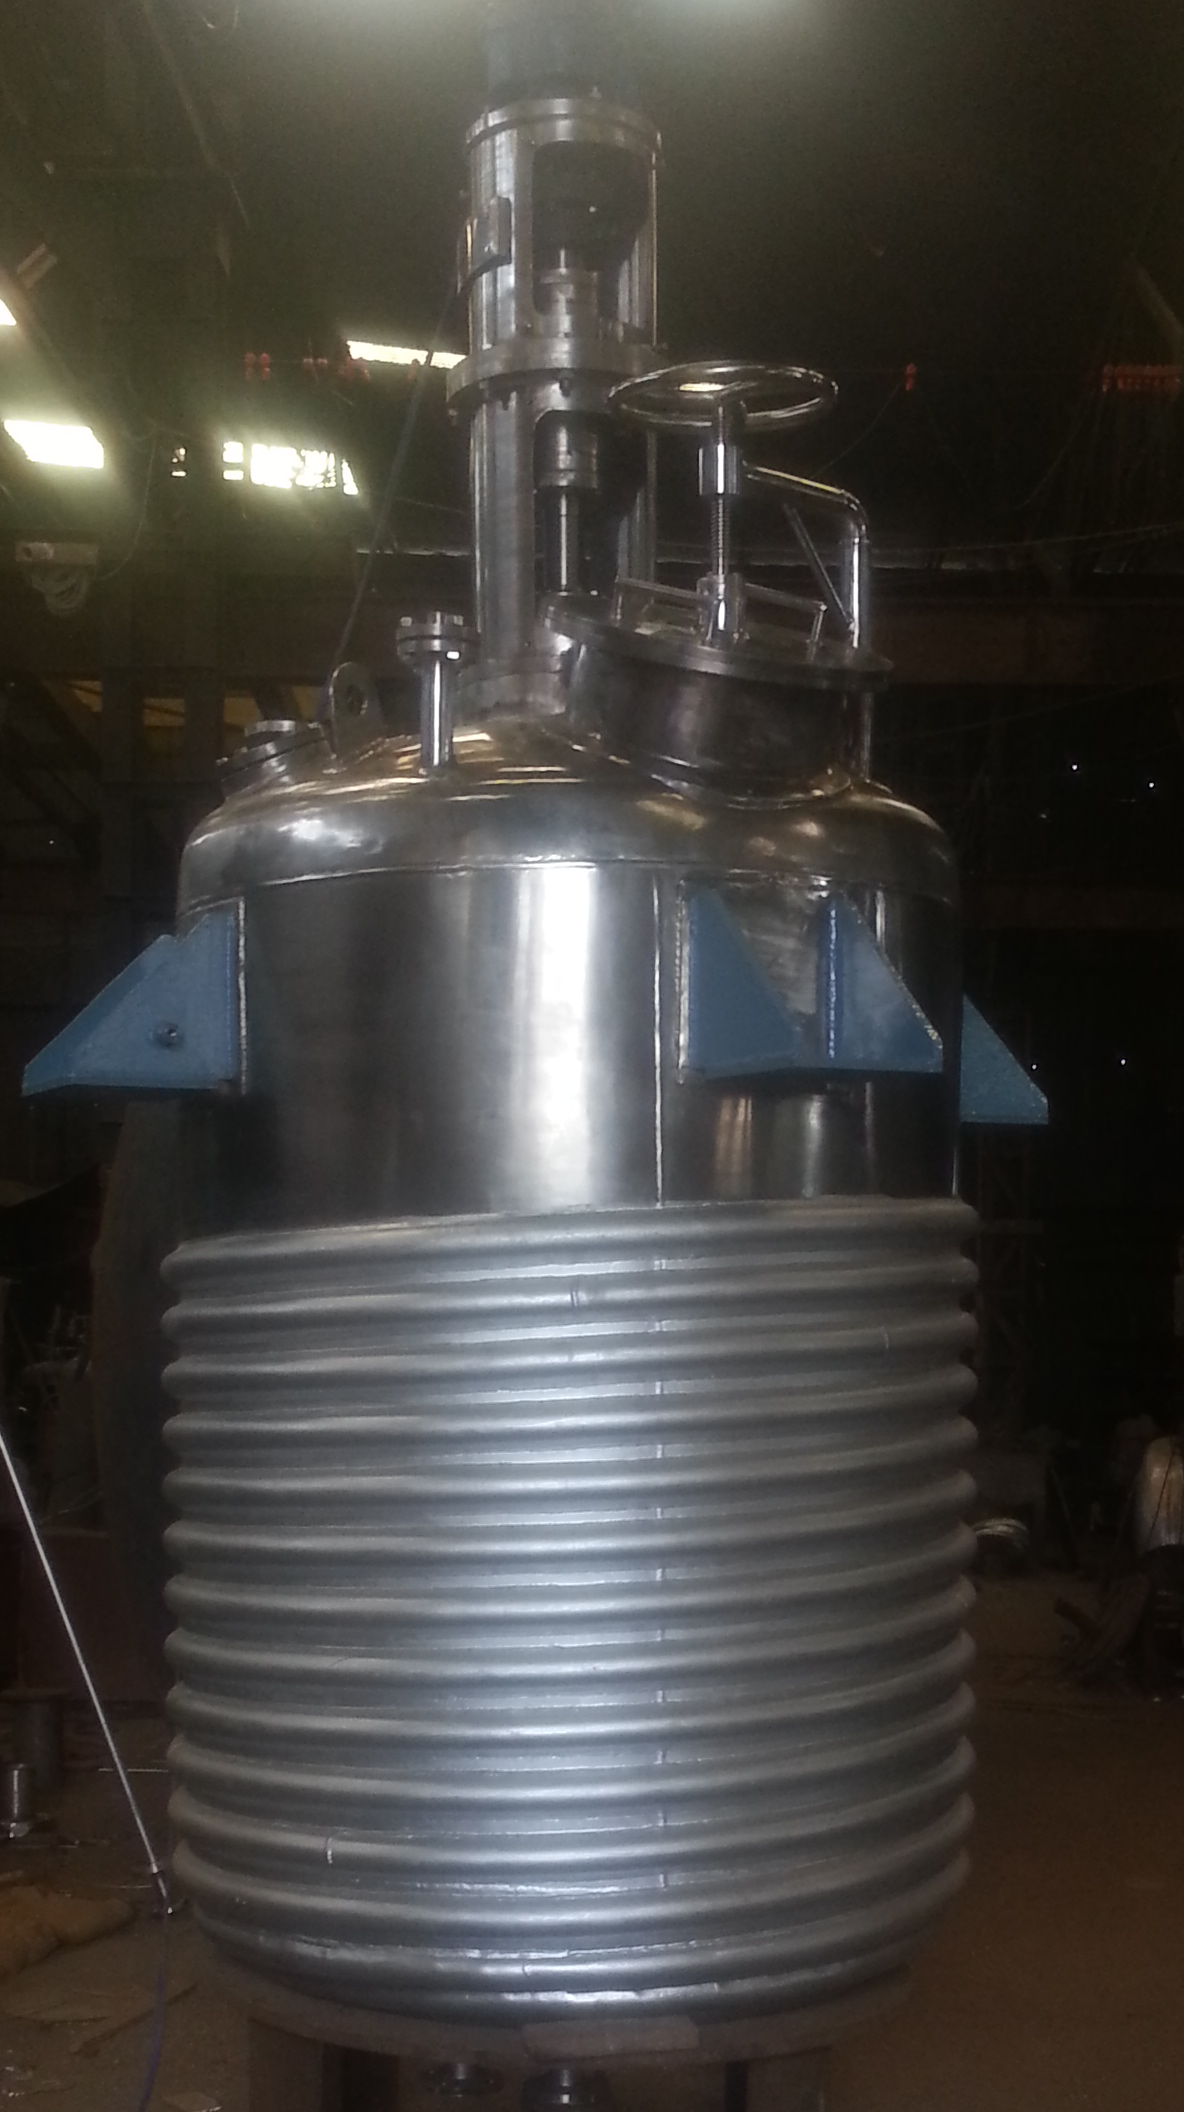
A chemical reactor is a closed process vessel in which raw materials (reactants) are mixed and reacted under controlled temperature, pressure and agitation. Febchem Engineering Pvt. Ltd. is a chemical reactor manufacturer, supplier and exporter based in Indore, India. Our reactors are built for mixing, reaction, crystallization, extraction and polymerization, with a vertical cylindrical shell and dished end closures.
How Does a Chemical Reactor Work? (Working Principle Explained)
The chemical reactor is based on a brilliant management of conditions such as temperature, pressure, and mixing in order to promote sought-after chemical reactions successfully. A shaft containing blades (agitator) is used inside the vessel to vigorously stir the reactants, and baffles are designed to prevent swirling and aid in contact between substances.
Reactor design can include jackets, limpet coils or high-pressure capability, depending on the reaction type and whether it runs at normal or elevated pressure
What are the Key Features of Our Chemical Reactors
- Durable Construction: Constructed using material like SS 304, SS 316L, MS, or SA-516 GR-70 to be durable.
- Flexible Sealing Capabilities: Seals may incorporate an oil seal, a water-cooled stuffing box, or a single/double mechanical seal to accommodate a range of pressures.
- Special Agitators: Select an anchor, PBT, Rushton turbine, propeller, or other agitator design, each specific to your application.
- Insulation & Cladding: On request, high-density glass wool insulation and stainless steel cladding are available.
- Large Capacity Range: Capacities up to 50 KL (50,000 liters), suitable for pilot-scale and full-scale production.
Chemical Reactors Technical Specifications
| Parameter | Specification |
| Capacity | upto 50 KL |
| MOC | SS-304, SS-316, MS, SA-516 Gr-70 |
| Design | Jacketed, Limpet |
| Max pressure | 25 bar |
| Max temp | 300 C |
| Stirrer type | Can be designed according to specifications |
| Heating | Thermic |
| Heating | Steam |
| Phase | 3 phase |
| Mounting | Platform |
| Orientation | Vertical |
Applications of Chemical Reactors in Industries
Chemical reactors are fundamental in the industry of:
- Chemical Production: Supports reactions, extraction, crystallization, polymerization, etc.
- Pharmaceutical: it is ideal in mixing the active ingredients and carrying out a reaction, as well as processing under an extreme condition.
- Food & Beverage: facilitates extraction or distillation in a controlled way.
- Specialty Processing: Processes used in this are processes such as solid dissolution or distillation, depending on the needs.
We customize every reactor to your process, capacity and material requirements.
Chemical Reactor Price in India (Latest Cost Guide)
A chemical reactor can cost as low as ₹2 lakh or up to more than ₹9 lakh depending on the size, material, special features (such as insulation or pressure settings), and customization.
As the best chemical reactor exporter and chemical reactor manufacturer, Febchem Engineering Pvt Ltd has competitive rates that suit the process of your needs. To get a correct and current quote, all you have to do is to contact our sales team.
Chemical Reactor Manufacturers & Supplier in India
Febchem Engineering Pvt. Ltd. is a chemical reactor manufacturer, supplier and exporter based in Indore, Madhya Pradesh. We design and fabricate vertical, platform-mounted reactors up to 50 KL for chemical, pharmaceutical and specialty processing plants.
Every reactor is built around your process. Choose the material of construction (SS 304, SS 316, MS or SA-516 Gr-70), a jacketed or limpet coil design, and thermic fluid or steam heating. Our reactors are rated up to 25 bar and 300°C, and the agitator is designed to suit your reaction and batch requirements.
We handle design, fabrication and dispatch for domestic plants and export orders. Alongside reactors, we supply agitators, industrial heat exchangers, dryers, filters and centrifuges, so you can source a complete process line from one manufacturer.
Frequently Asked Questions About Chemical Reactor
1. What is an industrial reactor?
An industrial reactor is a process vessel where chemical reactions are carried out under controlled temperature, pressure, and mixing conditions.
2. What reactors are used in the chemical industry?
The most common reactors include SS Reactors, Glass Lined Reactors (GLR), Mild Steel Reactors, Pressure Reactors, and Limpet Coil Reactors.
3. How do chemical reactors work?
Chemical reactors mix raw materials under controlled conditions to safely produce the desired chemical reaction and final product.
4. What is the difference between GLR and SSR?
A Glass Lined Reactor (GLR) offers excellent corrosion resistance, while a Stainless Steel Reactor (SSR) provides high strength and durability for various chemical processes.
5. How much does a chemical reactor cost?
The chemical reactor price depends on capacity, material, pressure rating, and customization. Contact the manufacturer for an exact quotation.
Get a Free Chemical Reactor Consultation & Quote
Need the Right Chemical Reactor Manufacturer for Your Process?
Share your reaction requirements and our engineers will recommend the most suitable chemical reactor for your application.
- Energy Efficient
- Low Steam Consumption
- SS 304/316
- High Concentration
- Custom Capacity
- Corrosion Resistant
📞 Get a Technical Proposal Within 24 Hours.